Fast Global Shipping
Bulk Discounts
Over 10,000+ Product Variations
Trusted by 100,000+ Customers
Hardened Steel Screw-Serts
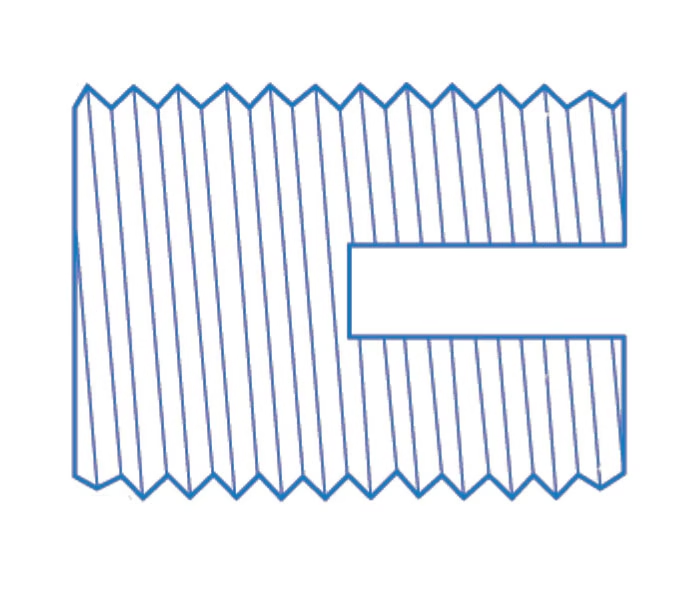
PSM Screw-Sert inserts are self-tapping metallic inserts designed to form their own threads in thermoplastic or thermoset materials, enabling a durable steel thread in plastics that otherwise may be too weak to hold repeated screw cycles. They are especially useful in applications where high pull-out loads, jack-out resistance, or weak core strength plastics are involved.
Advantages
- Easy press-in insertion
- Ideal where jack-out loading is unavoidable
- Can carry high loads in weak plastics
Key Features
- Self-tapping: no pre-tapped hole is needed; the insert cuts or broaches its own thread as it’s driven in
- High pull-out resistance: designed to resist being pulled from the plastic under load
- Excellent torque-out strength: capable of withstanding twisting or loosening forces
- High reusability: steel thread enables multiple screw cycles without degrading performance
- Accommodates weak plastics: suitable for substrates with limited core strength
- Flanged and stud versions available to suit different assembly geometries
Selection of Inserts
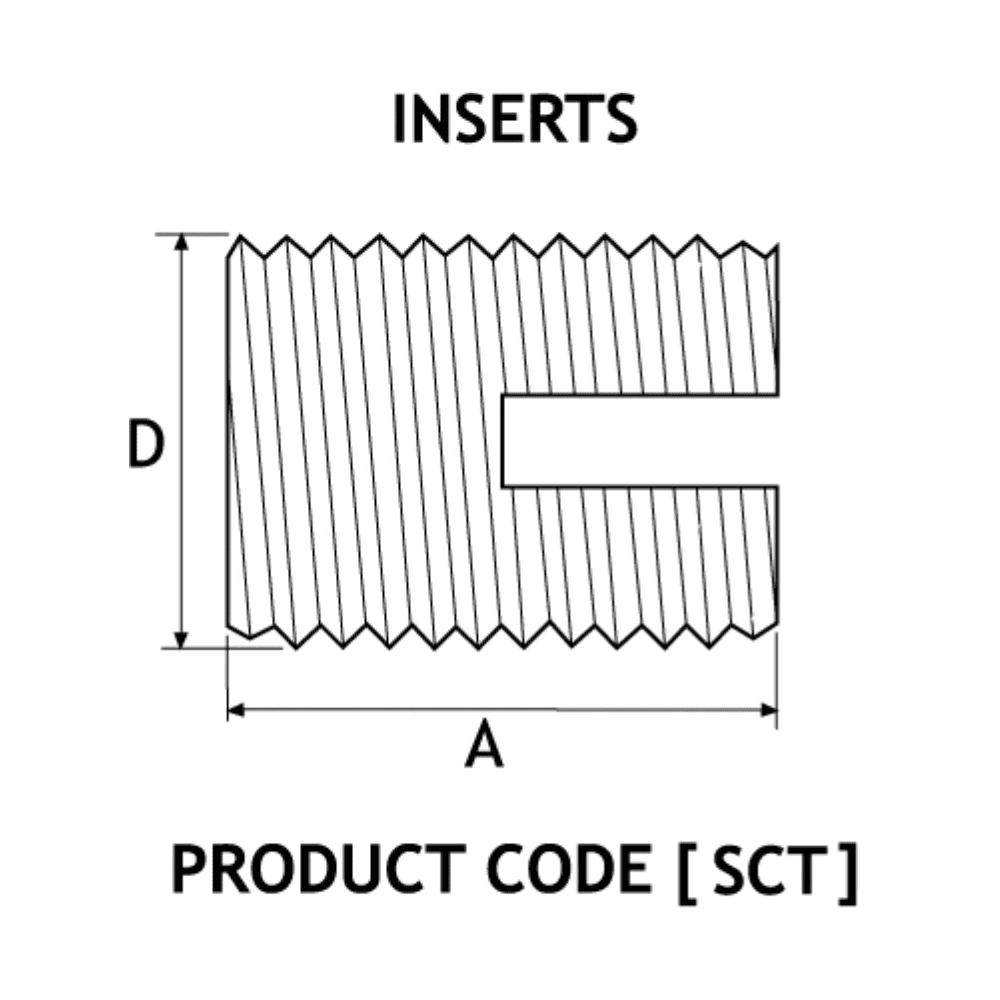
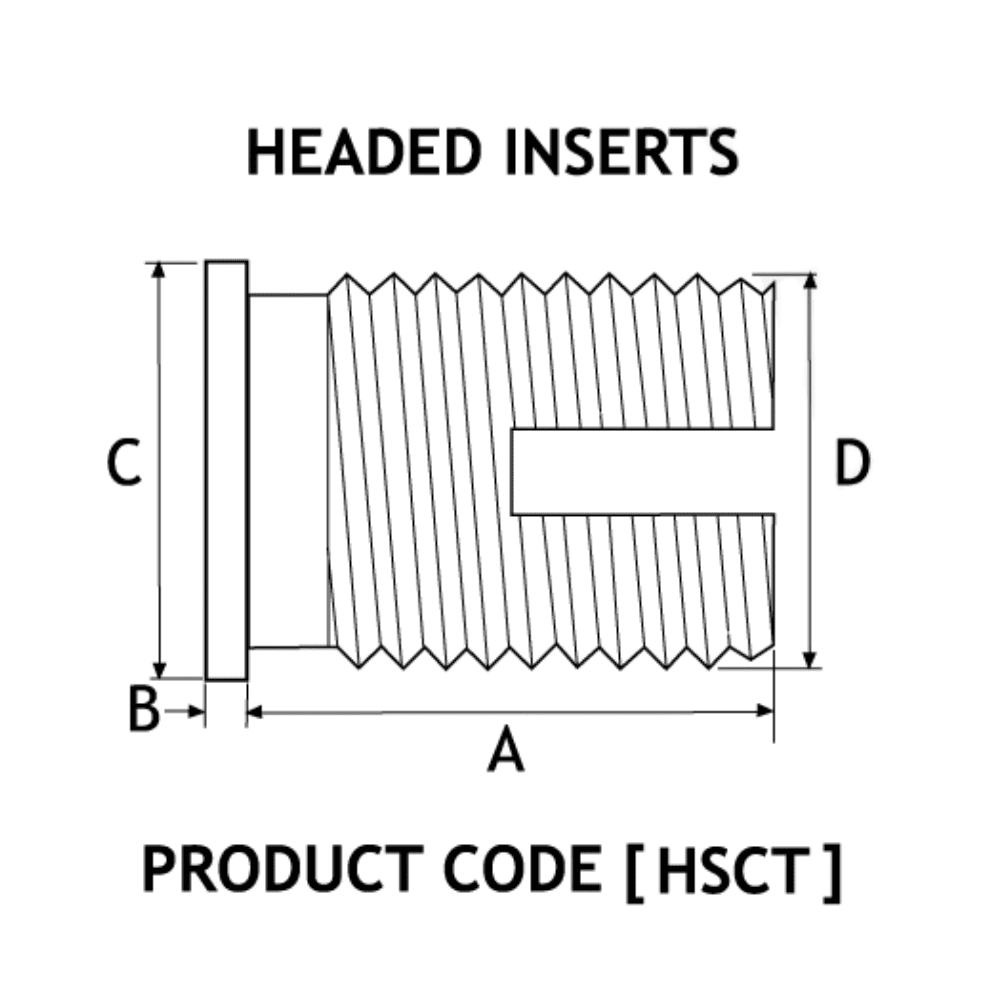
ISO Metric
| Nut Size | Material Thickness mm |
Cold Rolled Mild Steel | ||
|---|---|---|---|---|
| Push-out Kn |
Pull-out Kn |
Torque-out Nm |
||
| M5 | 0.7 | 3 | 4 | 9 |
| 1 | 7 | 7 | 9 | |
| 1.5 | 9 | 10 | 9 | |
| M6 | 0.7 | 3.9 | 4.7 | 19 |
| 1 | 7.3 | 7.4 | 19 | |
| 1.5 | 11.9 | 11 | 19 | |
| 2 | 14 | 11.5 | 19 | |
| M8 | 0.7 | 4.8 | 4.5 | |
| 1 | 6.5 | 9.7 | 36 | |
| 1.5 | 13.1 | 16 | 36 | |
| 2 | 17 | 16 | 36 | |
| 2.5 | 27.9 | 18 | 36 | |
| M10 | 1 | 7.3 | 9.6 | |
| 1.5 | 10.8 | 15.2 | 80 | |
| 2 | 16.7 | 20 | 81 | |
| 2.5 | 28 | 20 | 84 | |
| 3 | 29 | 20 | 86 | |
| M12 | 1.5 | 26 | 18 | 100 |
| 2 | 44 | 24 | 114 | |
| 2.5 | 44 | 28 | 140 | |
| 3 | 45 | 31 | 140 | |
Other lengths possible on quotation.
Unified
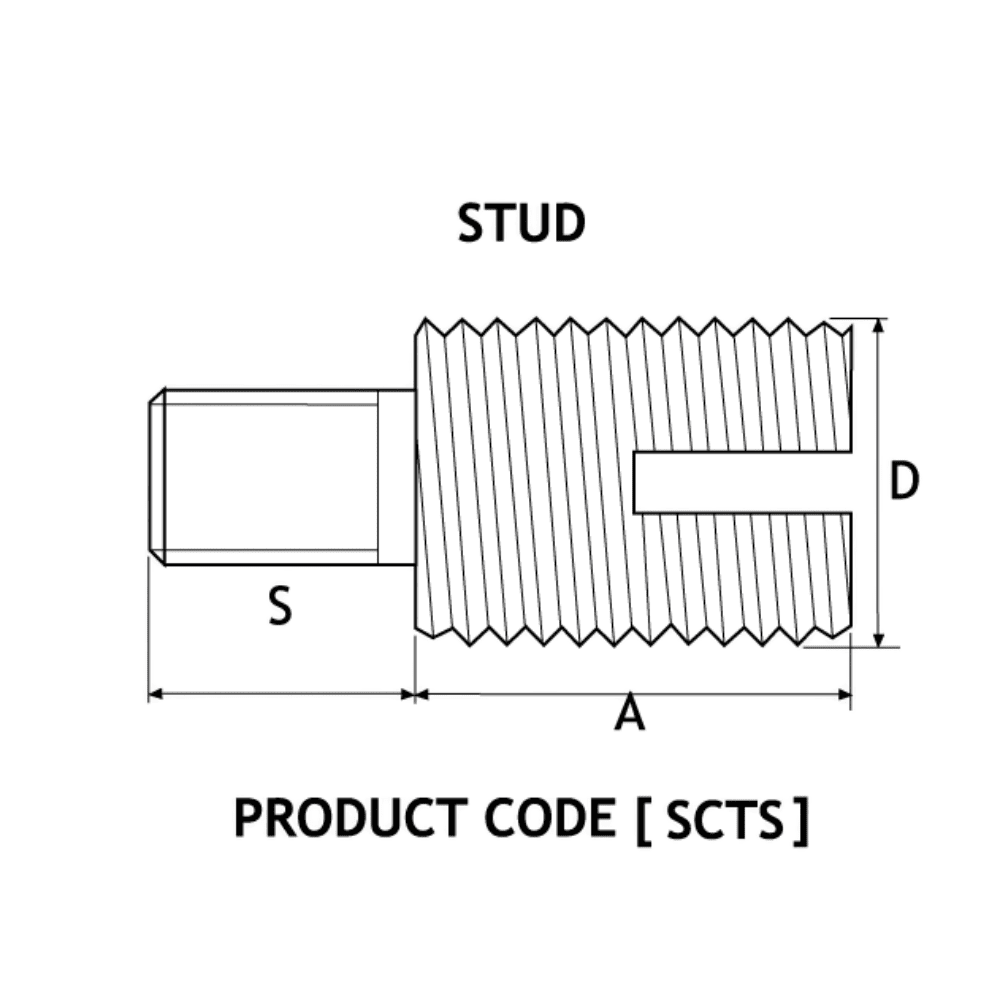
| PRODUCT CODE |
THREAD SIZE |
INSERT LENGTH A |
STUD LENGTH (FOR SCTS ONLY) S |
HEAD HEIGHT B |
HEAD Ø C |
INSERT Ø D MAX |
FOR THERMO
PLASTICS REC. HOLE SIZE -0.000 +0.004 |
REC. HOLE SIZE FOR THERMO SETTING -0.00 +0.10 |
MIN. WALL THICKNESS |
|||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
|
SCT-B HSCT-B SCTS-B |
2-56 | .236 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .023 | .236 | .177 | .157-.161 | .161-.169 |
EVALUATED BY PRE- PRODUCTION TESTS |
| 4-40 | .236 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .023 | .236 | .177 | .157-.161 | .161-.169 | ||
| 6-32 | .315 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .029 | .295 | .236 | .209-.213 | .217-.224 | ||
| 8-32 | .315 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .035 | .312 | .256 | .228-.232 | .217-.224 | ||
| 10-24 | .394 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .042 | .374 | .315 | .283-.283 | .287-.299 | ||
| 10-32 | .394 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .042 | .374 | .315 | .280-.283 | .287-.299 | ||
| 1/4-20 | .551 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .052 | .472 | .394 | .339-.346 | .354-.370 | ||
| 1/4-28 | .551 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .052 | .472 | .394 | .339-.346 | .354-.370 | ||
| 5/16-18 | .591 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .052 | .551 | .472 | .417-.425 | .433-.449 | ||
| 5/16-24 | .591 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .052 | .551 | .472 | .417-.425 | .433-.449 | ||
| 3/8-16 | .709 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .062 | .630 | .551 | .496-.504 | .512-.528 | ||
| 3/8-24 | .709 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .062 | .630 | .551 | .496-.504 | .512-.528 | ||
| 1/2 | .866 | 3/16 | 1/4 | 5/16 | 3/8 | 7/16 | 1/2 | 5/8 | 3/4 | 7/8 | 1 | .062 | .709 | .630 | .575-.583 | .591-.606 | ||
Other materials and lengths possible on quotation.
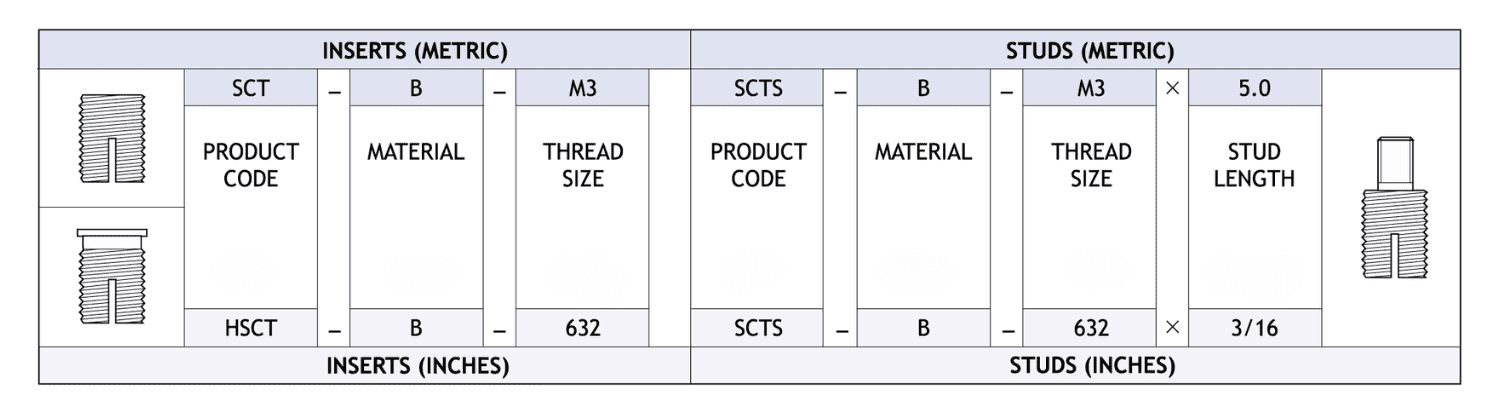
Specifying an Insert & Stud
Boss Design Specification
Hole Preparation
Hole diameter will vary with the type of plastic material used – hard plastics will require larger holes than softer plastics etc. For this reason, the data table shows the hole size ranges recommended for thermoplastics and thermosetting plastics. Exact hole size is best determined by pre-production trials – please consult the P.S.M Technology Centre. It is recommended that molded holes are used. A 60° countersink at the top of the hole is strongly recommended in order to avoid the risk of chipping to the surrounding surface. The depth of the countersink should be equal to the external thread pitch of the insert. Tapers on molded holes should be 1° inclusive.
Type of Loading
Direct torque loads should be avoided with this type of insert.
Installation
The insert is installed using traditional tapping principles. Installation can be carried out using a hand tool (for low volumes), a tapping head attachment for a pillar drill, a standard tapping machine or fully automatic installation equipment.
Wall Thickness
This must be evaluated by pre-production tests in conjunction with the PSM Technology Centre – contact your local sales office for advice.
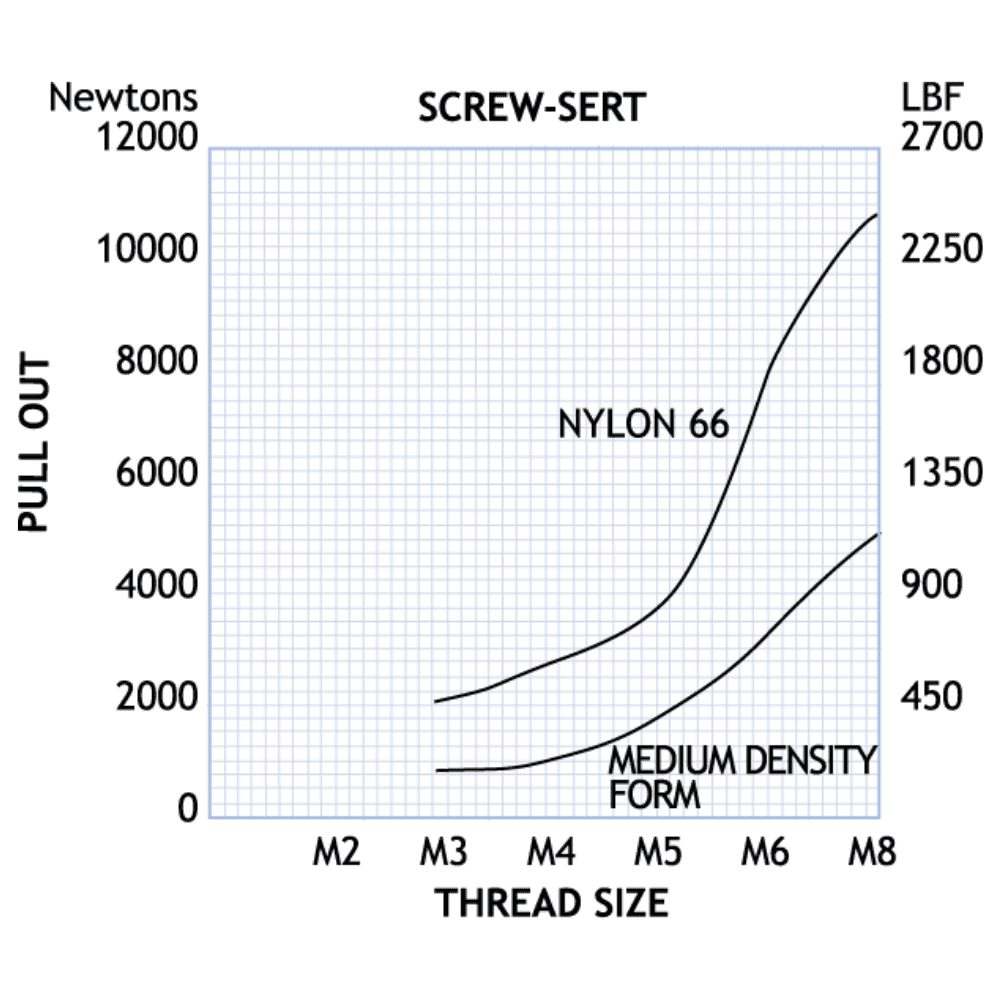
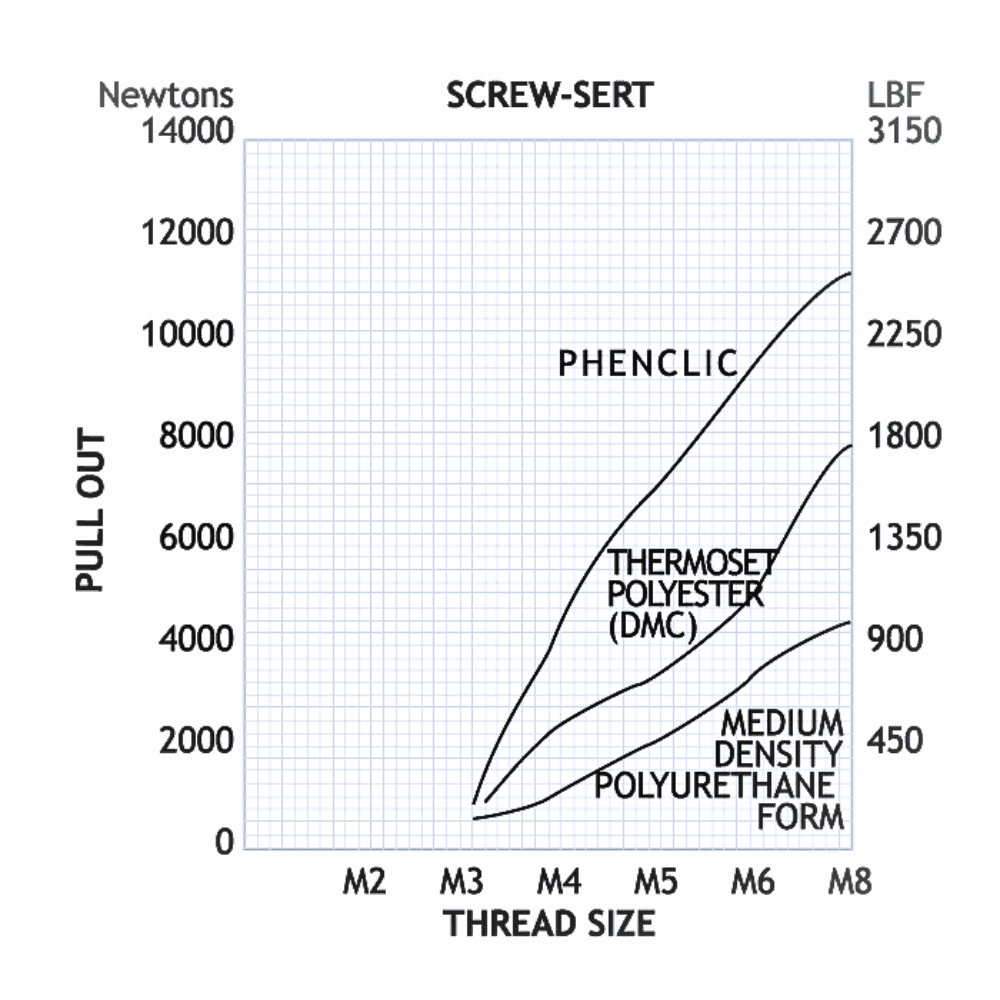
Performance Data
The complexity of materials and variations in service conditions make it impossible to detail fastener performance for specific applications. The charts below give a general guide and show the relative performance of the inserts in the range.
Enhance Your Assembly with Our Hardened Steel Screw Serts
Start browsing our products or request a quote today to find the ideal fastening solution for your application.
Frequently Asked Questions About Hardened Steel Screw-Serts
What is a hardened steel screw-sert?
How does a hardened steel screw-sert work?
What materials can hardened steel screw-serts be installed into?
What industries use hardened steel screw-serts?
Hardened steel screw-serts are used across a wide range of industries where fastening into hard or special materials is required:
- Automotive & motorsport — fastening into cast iron engine blocks, hardened gear housings, and sintered metal components
- Mining & heavy equipment — re-threading stripped or damaged threads in hardened wear parts
- Defence & aerospace — reliable threaded connections in high-strength, difficult-to-machine alloys
- Industrial machinery — thread repair and insert installation in hardened tool steel fixtures
- Electronics & precision engineering — fastening into ceramics and hard anodised aluminium
- General thread repair — restoring stripped threads in hardened components where re-tapping is not possible